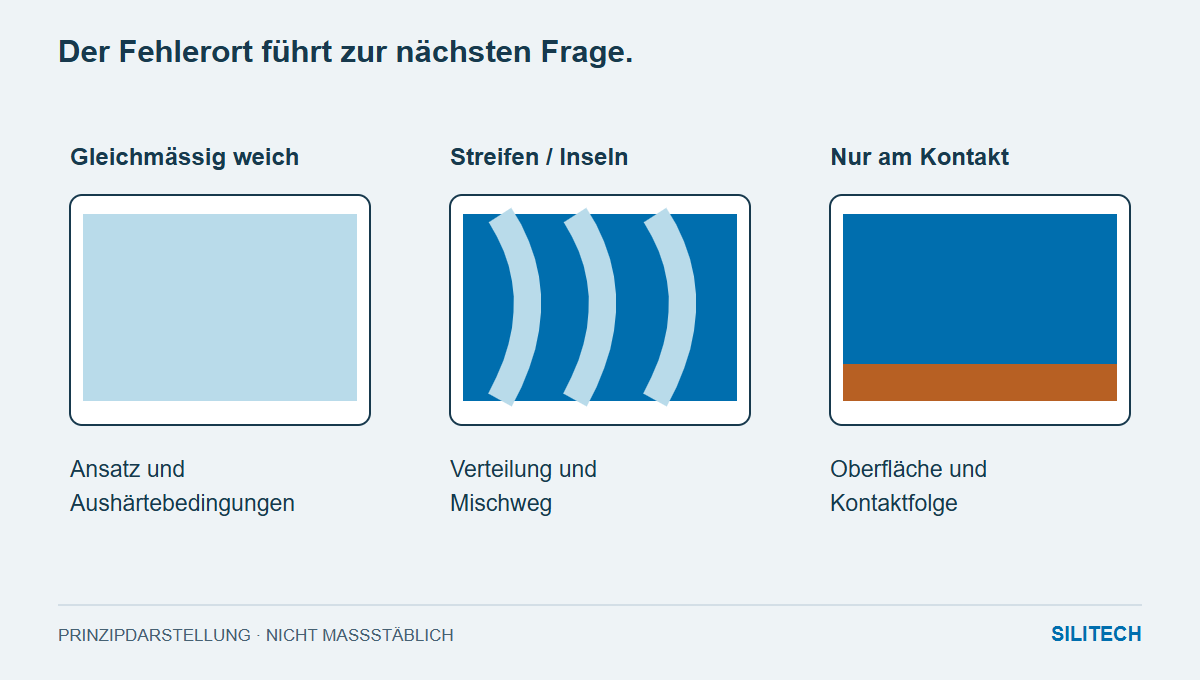
A potted part remains soft. The quick explanation is often: too little hardener. But an incorrect ratio is only one possible cause. Analyzing the distribution of the soft spots usually provides a better starting point.
First, the target state must be correct. Some potting materials remain elastic or gel-like. "Can be pressed in" is not a defect in these cases. A deviation only occurs if the material does not reach the state intended for this product under the corresponding curing conditions.
The entire approach is equally affected
Then it's worth taking a look at the weight of the components, the pair of components, and the temperature profile. Were the components the correct pair? Was the mixture dosed by mass or volume? Has the intended curing time even been reached?
A mix-up in the reference quantity can be subtle. For LOCTITE EA 9483, the specified resin-to-hardener ratio is 2:1 by volume, but 100:46 by mass. Therefore, 100 g of resin requires 46 g of hardener. Adding 50 g simply applies the volume ratio to the scale. The effect of this discrepancy isn't immediately apparent from this calculation; it primarily explains the dosing error.
Solid zones alternate with sticky strips
Here, the distribution of the components becomes paramount. The total quantities may be correct, yet the components may still not mix properly in each location. When mixing by hand, the bottom and sides of the mixing container require attention. If unmixed material is carried over from the sides during pouring, it will enter the component as a separate zone.
With a static mixer, the time course is helpful: Did the deviation occur at the start, after a pause, or during the entire discharge process? A combined sample from all samples obscures precisely this difference. Separate samples from the beginning and during the ongoing discharge process preserve it.
Only the surface on the component remains sticky
If the same mixture cures differently away from the contact surface, the surface should be investigated. With certain addition-curing silicones, contact materials can inhibit cross-linking. This is a different mechanism than an incorrect total weight. For other systems, other surface influences may be responsible.
The appropriate control test establishes the contact that is actually relevant: the same substrate with paint, cleaner, or release agent, plus material from the same batch on a known reference. Applying an additional coating on suspicion would initially create a new surface and postpone the original question.
The formula remains stable during troubleshooting
Adding extra hardener is not a general accelerator. Heat also does not replace the correct ratio or sufficient mixing. Post-curing is only appropriate if the specific system and assembly are designed for it.
The most helpful information for troubleshooting is an overview of the fault location along with the actual quantities and the temperature-time profile. This allows the next investigation to be narrowed down to dosage, distribution, or contact.
Two practical questions
Is a hard residue in the cup evidence to the contrary?
He is showing the condition of this sample. The thin joint or the potting compound on the component has different contact surfaces and possibly a different temperature profile. Both findings can be correct simultaneously.
May I change the ratio if the material hardens too slowly?
Only an explicit product-specific requirement can justify a different ratio. Otherwise, the intended process, including temperature and batch size, is considered first.
Mentioned in the article
LOCTITE EA 9483 - Highly transparent epoxy adhesive ↗To deepen the connection
The current product documentation is decisive for processing.