

 Silicones, silicone oils, sprays
 Casting and potting resins
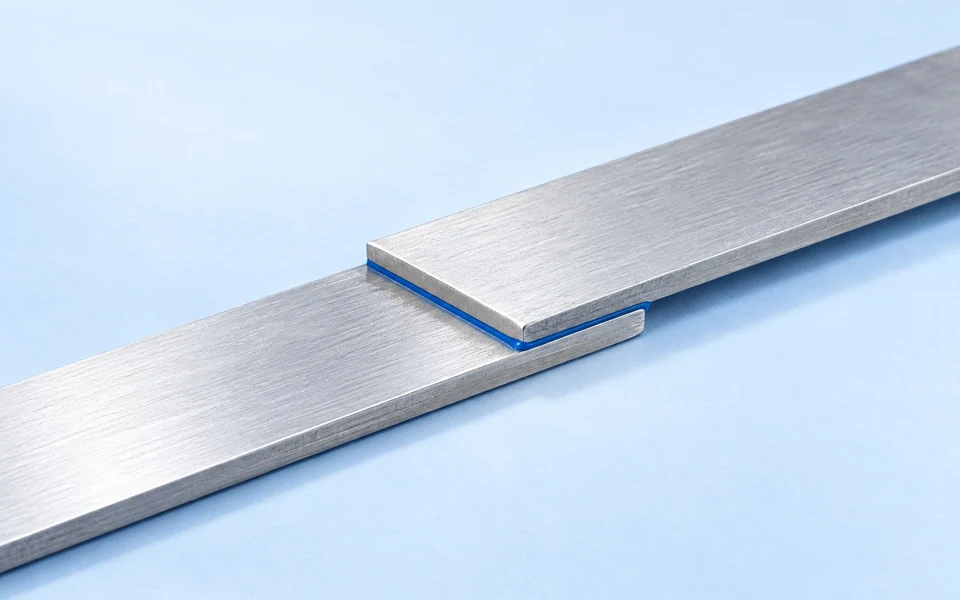
Two opaque metal parts need to be joined. The adhesive joint will be concealed later, leaving little time before the next assembly step. These specifications alone limit the choice of adhesive – even before comparing strength values.
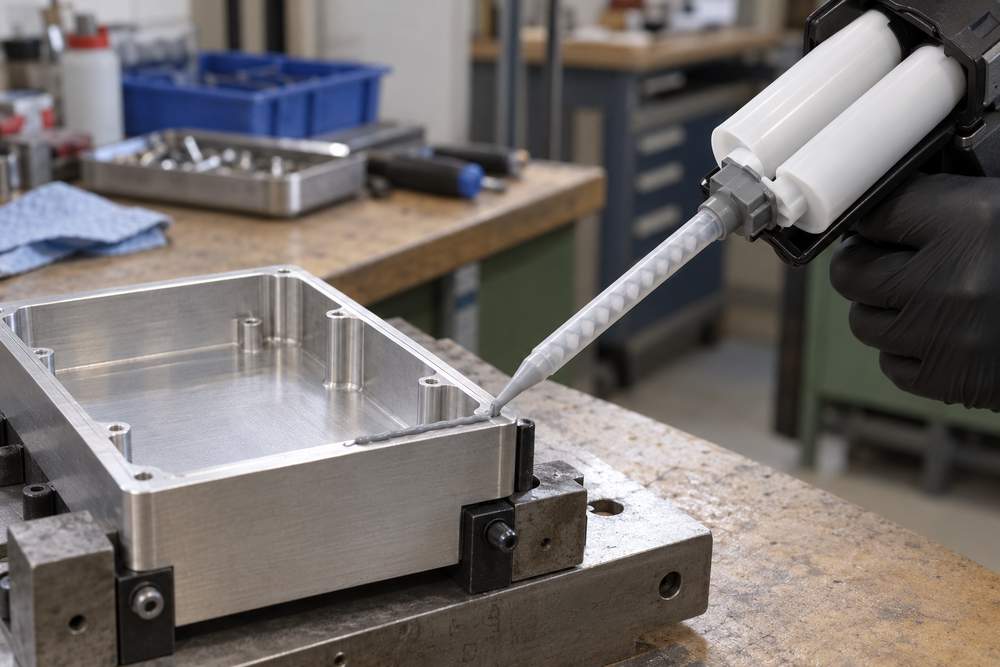
The first question is: What conditions trigger the curing process, and can these conditions be achieved across the entire joint? This leads to requirements regarding dosage, heat, light, positioning, and fixation.
Mixing or heat: Two different epoxy processes
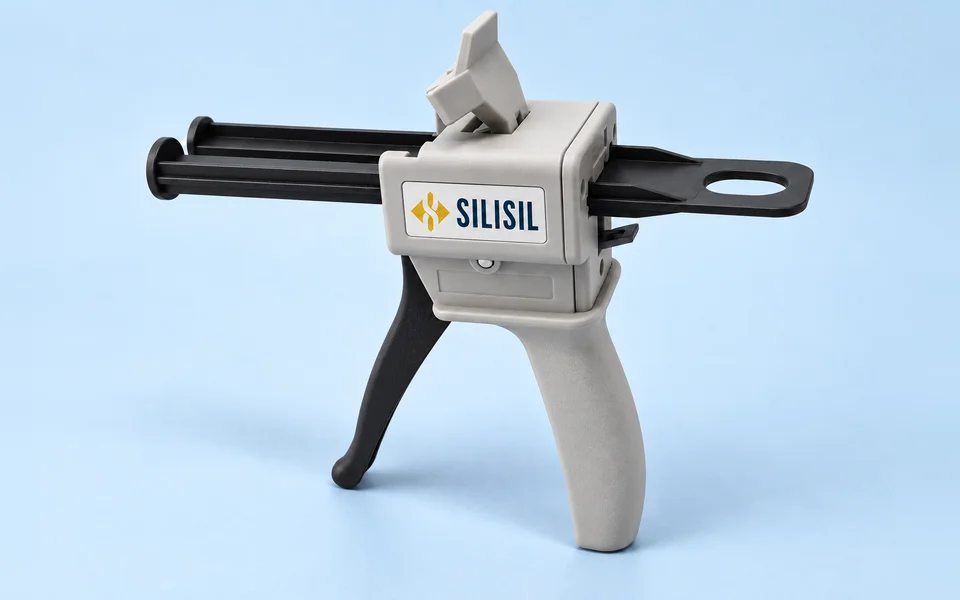
With two-component epoxy adhesives, the resin and hardener are mixed in the prescribed ratio. Permabond, for example, describes cartridges with static mixers and curing at room temperature. With appropriately designed products, heat can accelerate the curing process. Permabond: Two-component epoxies
For the metal parts, this becomes an assembly question: How does the mixture get into the gap, how long does the joining process take, and what device holds the position until the required strength is achieved? The product must be compatible with these steps.
With the group of thermosetting 1K epoxies , mixing immediately before application is unnecessary. Instead, the designated heating step is required. Therefore, whether the components and structure can withstand this step should be considered early in the selection process. Permabond: One-component epoxies
Rapid joining or metallic gap: CA and anaerobic systems
Cyanoacrylates harden upon contact with small amounts of moisture on their surfaces. Formulations and viscosities vary within this group. For assembly, the most important factor is how reliably the parts are aligned upon contact and what adjustments might still be necessary. Rapidly achieved strength is only beneficial if the desired position is reliably achieved. Permabond: Cyanoacrylates
For the anaerobic metal applications , suitable metal contact and exclusion of oxygen are among the curing conditions. Thread locking, thread sealing, and shaft-hub connections represent different tasks in this context. Permabond: anaerobic adhesives and sealants
Therefore, the joining gap is considered, not just the material name "metal". An exposed bead between two sheets must be assessed differently than a cylindrical fit. Surface finish, gap, and desired disassembly lead to the appropriate product question.
Light must reach the adhesive joint
For UV and light-curing adhesives, wavelength, intensity, and exposure time are all part of the process. Permabond describes several chemical systems and also products with an additional curing mechanism. Permabond: UV and light-curing adhesives
For the two opaque metal parts, the concealed area is crucial. An adhesive edge illuminated from the outside does not necessarily indicate that the entire joint is reached. Even with a component that appears transparent, it must be determined whether it allows the necessary light to pass through.
An additional mechanism can only resolve shadow areas if the selected product is designed for this purpose. The adhesive, component, and exposure unit together form the assembly to be tested.
The application method also plays a role in the case of structural acrylics
MMA-based adhesives belong to the structural acrylates. Permabond describes both two-component (2K) products, whose components are mixed before application, and no-mix processes with separately applied adhesive and initiator. Permabond: Structural acrylates
An existing mixing nozzle cannot be adopted solely based on its family name. First, the intended task must be clarified: premixing or separate contact surfaces, available time until joining, and appropriate dosage.
Only now should you compare strength and durability
After this initial selection, only the curing processes that make assembly possible remain. For their products, strength, temperature and media behavior are compared under comparable test conditions.
The component test ultimately connects the material and the process: intended surfaces, gap, load, and available equipment. It must demonstrate whether the connection fulfills its function and can be manufactured in this way.
Frequently asked questions
What specification narrows down the pre-selection more than "metal on metal"?
A sketch of the joint gap along with the possible curing steps. It shows, for example, whether light reaches the joint, whether a heat step is possible, and how the parts are held until they reach the required strength.
What needs to be clarified first when switching between two structural acrylates?
The application method. In the described no-mix method, the adhesive and initiator are applied separately; in the 2K method, the components are mixed beforehand. Dosage and assembly must be compatible.
Sources
- Permabond: two-part epoxies. Retrieved 2026-10-25.
- Permabond: single-part epoxies. Retrieved 2026-10-25.
- Permabond: cyanoacrylates. Retrieved 2026-10-25.
- Permabond: anaerobic adhesives. Retrieved 2026-10-25.
- Permabond: UV/light cure. Accessed 2026-10-25.
- Permabond: structural acrylics. Retrieved 2026-10-25.