

 Silicones, silicone oils, sprays
 Casting and potting resins
Internal Reference:
49-922.FL.G050
HS Code:
3506.9190000
Technical Data
Typical values, not a specification. The technical data sheet (TDS) is binding.
Product Information
- Manufacturer
- Permabond Engineering Adhesives Ltd
- Brand
- Permabond
- Container
- 50 g
- Country of origin
- Italy
Performance at Full Cure
- Impact strength (ASTM D-950)
- 3-5 kJ/m²
Physical Properties
- Color
- colorless
- Chemical group
- Allyl cyanoacrylate
- Viscosity (adhesives)
- Medium viscosity 500 - 5000 mPas
- Viscosity mPa.s
- 1200-2000
Curing values
- Maximum gap fill (mm)
- 0.4
- Fixture time on steel (sec.)
- <20
- Hand Strength Rubber (sec.)
- <15
- Hand Strength Phenol (sec.)
- <45
- Final strength
- 24 hours
Mechanical properties
- Hardness (Shore D)
- 85
Shear strength ISO 4587 in N/mm²
- Steel
- 19-23
Thermal Properties
- Storage Temperature (°C)
- 2-7
- Operating temperature (°C)
- -55 to +250
Product Description
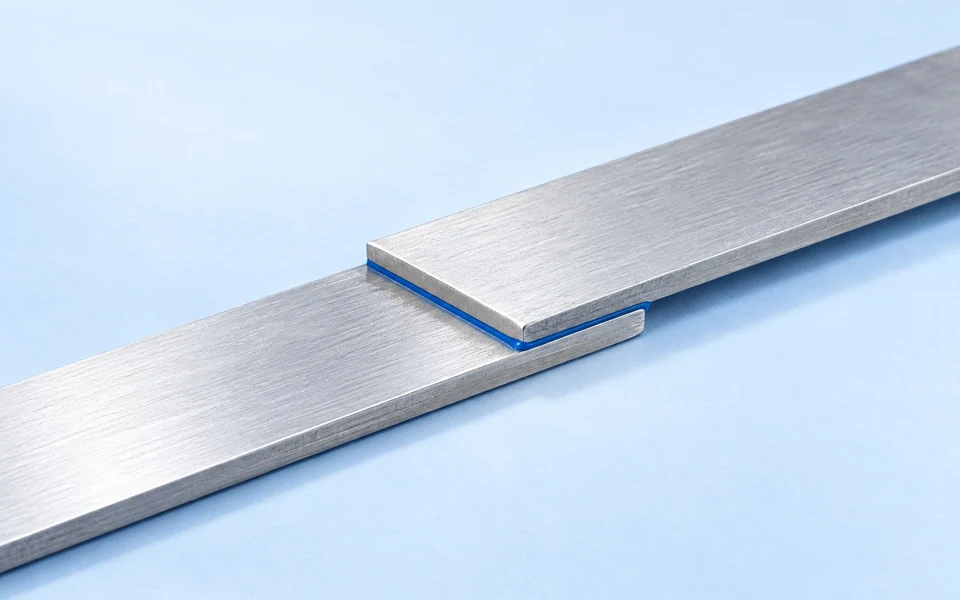
Permabond 922 is the high-viscosity allyl cyanoacrylate paste of the 919/920/922 series — paste consistency with 0.4 mm gap filling, designed for vertical high-temperature bonding and coarse tolerances, with post-cure permanently loadable up to 250 °C.
With 1,200 to 2,000 mPa·s, 922 is a true adhesive paste — it does not run, remains precisely where applied, and fills gaps up to 0.4 mm. This gap-filling capability is eight times greater than that of the ultra-low-viscosity 919, making 922 the first choice for coarse tolerances or vertical high-temperature bonding.
Like 919 and 920, 922 utilizes the two-stage post-cure process (4 h RT + 2 h 150 °C) for high-temperature performance up to 250 °C. The MIL-A-46050C Type V Class 3 approval is the high-viscosity classification of the MIL-Spec. Initial fixture strength on steel is achieved in under 20 seconds, and on phenolic in approximately 45 seconds.
MIL-A-46050C Type V Class 3 — the high-viscosity classification of the MIL-Spec. With two-stage post-cure curing (4 h RT + 2 h at 150 °C) permanently loadable up to 250 °C, combined with 0.4 mm gap filling — the unique paste variant of the allyl cyanoacrylate series.
What sets Permabond 922 apart
What is Permabond 922 used for?
Processing
Recommended accessories
Important Notes
Which Permabond for which application?
Permabond 922 in direct comparison with related cyanoacrylate products.
Permabond 922 Current Product | Permabond 919 → | Permabond 920 → | Permabond 737MM → | |
|---|---|---|---|---|
| Chemistry | Allyl cyanoacrylate | Allyl-CA | Allyl-CA | Ethyl-CA (toughened) |
| Viscosity | 1,200–2,000 mPa·s (paste) | 2–6 mPa·s | 80 mPa·s | 2,000–4,000 mPa·s |
| Max. gap fill. | 0.4 mm | 0.05 mm | 0.15 mm | 0.5 mm |
| Finger-tight on steel | <20 s | <20 s | 15–20 s | 15–20 s |
| Shear strength steel | 19-23 N/mm² | 20–22 N/mm² | 19-23 N/mm² | 19-23 N/mm² |
| Strength / Recommended for | Gap fill 0.4 mm | Ultra-low, MIL Class 1, wicking | Medium viscosity, MIL Class 2 + Bio | Black paste, without post-cure |
Frequently asked questions about Permabond 922
Practical application and design questions — answered by SILITECH.
Permabond 922 is an allyl cyanoacrylate instant adhesive with a viscosity of 1,200–2,000 mPa·s (paste) and a maximum gap fill of 0.4 mm. Allyl cyanoacrylate paste — MIL Class 3, 0.4 mm gap fill, with post-cure up to 250 °C.
Permabond 922 reliably bonds steel (19–23 N/mm²), as well as Buna-N rubber and similar elastomers. For polypropylene (PP), polyethylene (PE), PTFE, and silicone, pretreatment with Permabond Polyolefin Primer (POP) is required.
Permabond 922 is approved according to MIL-A-46050C Type V Class 3 (existing designs) — qualified for demanding industrial applications.
Permabond 922 achieves handling strength on steel in <20 s. Other typical cure times: <15 s (NBR), <45 s (Buna N), <45 s (Phenolic). Final strength of 19–23 N/mm² (steel) is reached after 24 hours. Temperature, humidity, and substrate affect the cure speed.
Permabond 922 offers a viscosity of 1,200–2,000 mPa·s (paste), a gap fill of 0.4 mm, and a shear strength of 19–23 N/mm² on steel. Permabond 919 has a viscosity of 2–6 mPa·s, a gap fill of 0.05 mm, and a shear strength of 20–22 N/mm² on steel (ultra-low, MIL Class 1, wicking). Both utilize an allyl cyanoacrylate base (or a related cyanoacrylate variant).
Permabond 922 should be stored unopened in a cool place at 2 to 7 °C and remains stable until the printed expiration date. Before opening, allow the bottle to warm to room temperature — this prevents condensation inside that would reduce shelf life. Opened bottles remain functional for several months when stored correctly, although cure speed may diminish over time. Before critical production use, we recommend a test bond to check reactivity.
From the Permabond cyanoacrylate series, select based on viscosity and special properties: Permabond 922 (1,200–2,000 mPa·s (paste), 0.4 mm gap width, gap filling); Permabond 919 (2–6 mPa·s, 0.05 mm, ultra-low, MIL Class 1, wicking); Permabond 920 (80 mPa·s, 0.15 mm, medium viscosity, MIL Class 2 + Bio); Permabond 737MM (2,000–4,000 mPa·s, 0.5 mm, black paste, no post-cure). For polypropylene, polyethylene, PTFE, and silicone, pretreatment with Permabond Polyolefin Primer (POP) is always required.