

PERMABOND HM 165
Permabond HM 165 — UV/light-activated adhesive.
Permabond HM165 — High-strength, high-viscosity shaft-hub adhesive (paste).
Documents
Internal reference:
49-200.FL.ML200
HS code:
3506.9190000
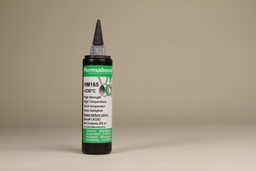
Permabond HM165 is a high-strength anaerobic shaft-hub adhesive in paste form — designed for fits with coarser tolerances down to 0.3 mm and the highest static torque requirements (35 N·m breakaway torque).
With a viscosity of 25,000 mPa·s, HM165 is truly pasty — it stays precisely where it is applied and fills large shaft-hub tolerances down to 0.3 mm. The paste consistency allows the shaft to be coated before being inserted into the hub.
The highest breakaway torque of 35 N·m in the anaerobic shaft-hub series makes HM165 the ideal choice for highly static bonded joints—such as fixing drive journals, hubs, or gear mounting. Disassembly typically requires heating the joint.
High-strength shaft-hub paste with the highest breakaway torque in the anaerobic series (35 N·m). A paste consistency of 25,000 mPa·s fills gaps up to 0.3 mm and remains stable even in rough fits.
What makes Permabond HM165 stand out
What is Permabond HM165 used for?
Processing
Recommended accessories
Important Notes
Which Permabond anaerobic adhesive for which application?
Permabond HM165 in direct comparison with related products of the A series.
Permabond HM165 Current Product | Permabond HM162 → | Permabond HM163 → | Permabond A1046 → | |
|---|---|---|---|---|
| Application / Strength | High-strength, high-viscosity shaft-hub adhesive (paste) | Low viscosity, tightly tolerated | Medium viscosity | A-Series Comparison |
| Viscosity | 25,000 mPa·s @ 2 rpm (paste) | 1,000 mPa·s | 3,500 mPa·s | Medium |
| Max. gap fill. | 0.3 mm | 0.2 mm | 0.2 mm | 0.25 mm |
| Breakaway Torque | 35 N·m | 32 N·m | 30 N·m | 30 N·m |
| Prevailing torque | 50 N·m | 57 N·m | 55 N·m | 50 N·m |
Technical data for PERMABOND HM 165
| Product Information | |
|---|---|
| Manufacturer | Permabond Engineering Adhesives Ltd |
| Brand | Permabond |
| Container | 200 ml |
| Country of origin | Italy |
| UFI (Unique Formula Identifier) | 7U50-C0DW-K002-N5TA |
| Performance at Full Cure | |
|---|---|
| Torque strength (M10 steel ISO10964) Breakloose | 35 Nm |
| Torque strength (M10 steel ISO10964) Prevailing | 50 Nm |
| Shear strength (steel ISO10123) | 20 MPa |
| Dielectric Strength | 11 kV/mm |
| Thermal conductivity | 0.19 W/(m.K) |
| Physical Properties | |
|---|---|
| Chemical group | Acrylic one-component |
| Viscosity 2rpm | 25000 |
| Viscosity at 20 rpm | 10000 |
| Color | green |
| Specific Gravity | 1.1 |
| Fluorescence | Yes |
| Curing values | |
|---|---|
| Handling strength (M10 steel)@23°C | 15-20 minutes |
| Functional strength (M10 steel)@23°C | 3-6 hours |
| Ultimate strength (M10 steel)@23°C | 24 hours |
| Thermal Properties | |
|---|---|
| Operating temperature (°C) | -55 to 230 |
| Storage Temperature (°C) | 5-25 |
| Coefficient of thermal expansion | 90 x 10-6 mm/mm/°C |
| General | |
|---|---|
| Gap fill up to | 0.3mm |
Please refer to the technical data sheet (TDS) in the "Documents" tab for binding values.
Documents and data sheets
Click on a document for the preview or the download icon for direct download.
Technical Data Sheets (TDS) 6
Frequently asked questions about Permabond HM165
Practical application and design questions — answered by SILITECH.
Permabond HM165 is an anaerobic acrylic adhesive with a viscosity of 25,000 mPa·s @ 2 rpm (paste) and gap filling capability up to 0.3 mm. This high-strength shaft-hub paste boasts the highest breakaway torque in the series (35 N·m) and is suitable for rough fits up to 0.3 mm. Anaerobic adhesives cure in the absence of air and metal-to-metal contact, making them ideal for tight-tolerance metal-to-metal bonds.
Anaerobic adhesives like Permabond HM165 remain liquid in the bottle (due to contact with air and oxygen) and only begin to harden after bonding under anaerobic conditions and metal-to-metal contact. Curing starts at the metal surface and progresses into the bond gap. The product cures quickly on steel and copper; on stainless steel and zinc, the Permabond A905 activator may be beneficial.
Difficult to remove — Permabond HM165 is high-strength (35 N·m breakaway torque). Disassembly typically requires heating the bond to 200 °C or more. Designed for permanent bonding.
Permabond HM165 does not have specific industry approvals such as WRAS or KTW (drinking water). For general industrial applications, the product is approved according to Permabond's internal specifications; however, product-specific testing prior to series production is recommended.
Permabond HM165 typically reaches handling strength after 15 minutes and functional strength after 1 hour at 23 °C on M10 steel. Final strength is reached after 24 hours. On inactive surfaces (stainless steel, zinc) or at low temperatures, the curing time is extended—Permabond A905 activator accelerates the process.
Permabond HM165 is a high-strength, high-viscosity shaft-hub adhesive (paste) (25,000 mPa·s @ 2 rpm (paste) viscosity, 0.3 mm gap filling, 35 N·m breakaway torque). Permabond HM162 is a high-strength, low-viscosity adhesive (1,000 mPa·s, 0.2 mm gap filling, 32 N·m breakaway torque) — low viscosity, tightly toleranced. Both belong to the anaerobic Permabond A series.
The choice depends on the application: Permabond HM165 (high-strength, high-viscosity shaft-hub adhesive (paste)); Permabond HM162 (high-strength, low-viscosity); Permabond HM163 (high-strength, medium-viscosity); Permabond A1046 (high-strength A-series). For inactive surfaces (stainless steel, zinc, aluminum), Permabond A905 activator should also be used to accelerate curing.
Your question not covered?
Our technical team provides personal advice on material selection, processing questions, and individual requirements. Fast and competent.
Product Specifications
| Product Information | |
|---|---|
| Manufacturer | Permabond Engineering Adhesives Ltd |
| Brand | Permabond |
| Container | 200 ml |
| Country of origin | Italy |
| UFI (Unique Formula Identifier) | 7U50-C0DW-K002-N5TA |
| Performance at Full Cure | |
|---|---|
| Torque strength (M10 steel ISO10964) Breakloose | 35 Nm |
| Torque strength (M10 steel ISO10964) Prevailing | 50 Nm |
| Shear strength (steel ISO10123) | 20 MPa |
| Dielectric Strength | 11 kV/mm |
| Thermal conductivity | 0.19 W/(m.K) |
| Physical Properties | |
|---|---|
| Chemical group | Acrylic one-component |
| Viscosity 2rpm | 25000 |
| Viscosity at 20 rpm | 10000 |
| Color | green |
| Specific Gravity | 1.1 |
| Fluorescence | Yes |
| Curing values | |
|---|---|
| Handling strength (M10 steel)@23°C | 15-20 minutes |
| Functional strength (M10 steel)@23°C | 3-6 hours |
| Ultimate strength (M10 steel)@23°C | 24 hours |
| Thermal Properties | |
|---|---|
| Operating temperature (°C) | -55 to 230 |
| Storage Temperature (°C) | 5-25 |
| Coefficient of thermal expansion | 90 x 10-6 mm/mm/°C |
| Uncategorized | |
|---|---|
| Gap fill up to | 0.3mm |
| Keywords | |
|---|---|
| Keywords | |
Documents and data sheets
Safety Data Sheets (SDS) and Technical Data Sheets (TDS) for download:
- Permabond HM 165 - Technical Data Sheet FR.pdf (459 KB)
- Permabond HM 165 - Technical Data Sheet FR.pdf (298 KB)
- Permabond HM 165 - Fiche de Sécurité FR.pdf (346 KB)
- Permabond HM 165 - Safety Data Sheet EN.pdf (342 KB)
- Permabond HM 165 - Safety Data Sheet DE.pdf (364 KB)
- Permabond HM 165 - Technical Data Sheet EN.pdf (504 KB)
- Permabond HM 165 - Technical Data Sheet EN.pdf (344 KB)
- Permabond HM 165 - Technical Data Sheet DE.pdf (478 KB)
- Permabond HM 165 - Technical Data Sheet DE.pdf (327 KB)