)
)
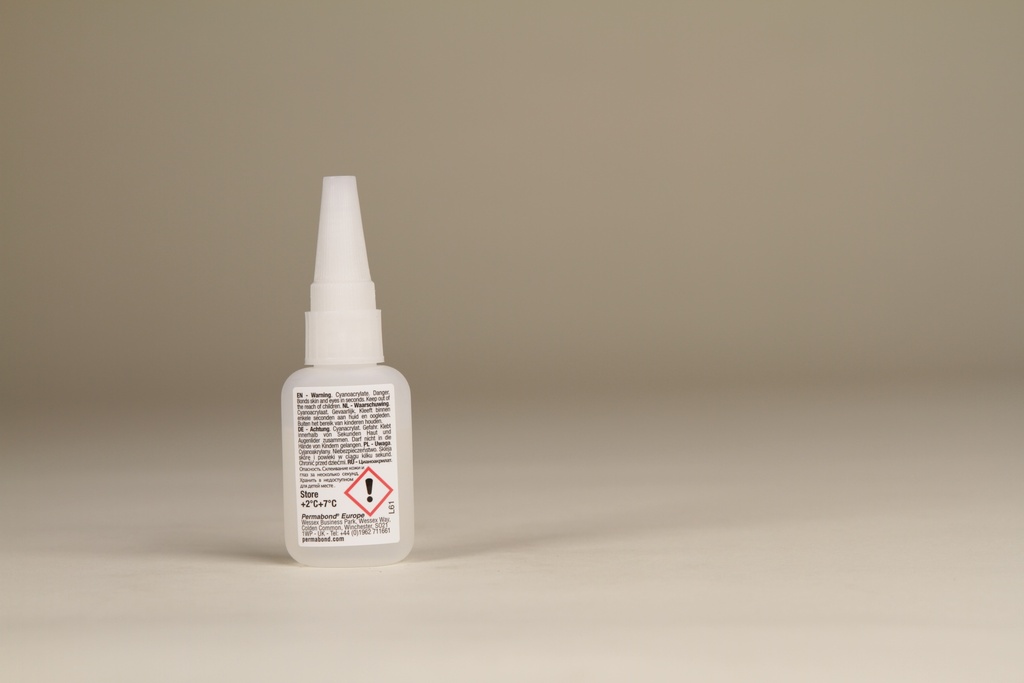
PERMABOND 791
Superglue, ultra-low viscosity, MIL-A-46050C Class 1
MIL-A-46050C Class 1 approved — the Wicking adhesive for micro gaps and post-production precision fixing.
Documents
Internal reference:
49-791.FL
HS code:
3506.9190000

Permabond 791 is an ultra-low viscosity ethyl cyanoacrylate adhesive optimized for wicking applications, micro gaps and the subsequent bonding of pre-joined precision components — qualified to MIL-A-46050C Class 1.
With a viscosity of 15–50 mPa·s, 791 is in the ultra-low viscosity range. The liquid penetrates micro-gaps and already assembled components via capillary action—a process known as wicking—and hardens to hand strength within 2 to 3 seconds.
The MIL-A-46050C Class 1 approval qualifies 791 for industrial, aerospace, and defense applications. On ABS, PVC, and polycarbonate, the break test results in substrate failure—the bond is stronger than the substrate. The maximum gap filling of 0.1 mm is designed for tight tolerance fits.
MIL-A-46050C Type II Class 1 (existing designs) & CID AA-3097 Type II Class 1 (new designs) — the most important international specification for cyanoacrylate industrial adhesives. Qualified for industrial, aerospace, and defense applications.
What distinguishes Permabond 791
What is Permabond 791 used for?
Processing
Recommended accessories
Important Notes
Which Permabond for which application?
Permabond 791 in direct comparison with related cyanoacrylate products.
Permabond 791 Current Product | Permabond 792 → | Permabond 712 → | Permabond 801 → | |
|---|---|---|---|---|
| Chemistry | Ethyl Cyanoacrylate | Ethyl-CA | Ethyl-CA | Ethyl-CA |
| Viscosity | 15-50 mPa·s | 60–125 mPa·s | 100 mPa·s | 10–15 mPa·s |
| Max. gap fill. | 0.1 mm | 0.15 mm | 0.15 mm | 0.05 mm |
| Finger-tight on steel | 2–3 s | 2–3 s | 25 s | 10–15 s |
| Shear strength steel | 18-22 N/mm² | 18-22 N/mm² | 19–24 N/mm² | 19–23 N/mm² |
| Strength / Recommended for | Class 1 approved MIL | MIL Class 2 + NSF Standard | Hot/Wet, 120 °C | High temperature |
Technical data for PERMABOND 791
| Product Information | |
|---|---|
| Manufacturer | Permabond Engineering Adhesives Ltd |
| Brand | Permabond |
| Container | 20 g, 50 g, 500 g |
| Country of origin | Italy |
| Tensile Strength | >20 N/mm² |
| UFI (Unique Formula Identifier) | Y5H0-3'7J-A00F-14R2 |
| Performance at Full Cure | |
|---|---|
| Shear strength polycarbonate | >6 |
| Dielectric strength | 25 kV/mm |
| Physical Properties | |
|---|---|
| Color | colorless |
| Chemical group | Ethyl Cyanoacrylate |
| Viscosity (adhesives) | Low viscosity <500 MPas |
| Viscosity mPa.s | 15-50 |
| Curing values | |
|---|---|
| Maximum gap fill (mm) | 0.1 |
| Fixture time on steel (sec.) | 2-3 |
| Hand Strength Rubber (sec.) | 2-3 |
| Hand Strength Phenol (sec.) | 2-3 |
| Final strength | 24 hours |
| Mechanical properties | |
|---|---|
| Hardness (Shore D) | 85 |
| Shear strength ISO 4587 in N/mm² | |
|---|---|
| Steel | 18-22 |
| ABS | >6 |
| PVC | >10 |
| Thermal Properties | |
|---|---|
| Operating temperature (°C) | -55 to +80 |
| Storage Temperature (°C) | 2-7 |
Please refer to the technical data sheet (TDS) in the "Documents" tab for binding values.
Documents and data sheets
Click on a document for the preview or the download icon for direct download.
Technical Data Sheets (TDS) 3
Frequently asked questions about Permabond 791
Practical application and design questions — answered by SILITECH.
Permabond 791 is an ethyl cyanoacrylate instant adhesive with a viscosity of 15–50 mPa·s and a maximum gap filling of 0.1 mm. Ultra-low viscosity cyanoacrylate adhesive — MIL-A-46050C Class 1, wicking-capable.
Permabond 791 reliably bonds steel (18–22 N/mm²), ABS (>6 N/mm² (substrate failure)), PVC (>10 N/mm² (substrate failure)), polycarbonate (>6 N/mm² (substrate failure)), as well as Buna-N rubber and similar elastomers. For polypropylene (PP), polyethylene (PE), PTFE, and silicone, pretreatment with Permabond Polyolefin Primer (POP) is required.
Permabond 791 is approved according to MIL-A-46050C Type II Class 1 (existing designs), CID AA-3097 Type II Class 1 (new designs) — qualified for demanding industrial applications.
Permabond 791 reaches handling strength on steel in 2–3 seconds. Other typical curing times: 2–3 seconds (Buna N), 2–3 seconds (phenol). The final strength of 18–22 N/mm² (steel) is reached after 24 hours. Temperature, humidity, and substrate affect the curing rate.
Permabond 791 offers a viscosity of 15–50 mPa·s, 0.1 mm gap filling, and 18–22 N/mm² shear strength on steel. Permabond 792 has a viscosity of 60–125 mPa·s, 0.15 mm gap filling, and 18–22 N/mm² shear strength on steel (MIL Class 2 + NSF, standard). Both utilize an ethyl cyanoacrylate base (or a related cyanoacrylate variant).
Permabond 791 should be stored unopened at 2 to 7 °C and is stable until the printed expiration date. Allow the bottle to warm to room temperature before opening—this prevents condensation inside, which would reduce its shelf life. Opened bottles remain functional for several months if stored correctly, although the curing rate may decrease over time. We recommend a test bond to check reactivity before critical production applications.
From the Permabond cyanoacrylate range, select according to viscosity and special properties: Permabond 791 (15–50 mPa·s, 0.1 mm gap width, Class 1 approved); Permabond 792 (60–125 mPa·s, 0.15 mm, MIL Class 2 + NSF, standard); Permabond 712 (100 mPa·s, 0.15 mm, hot/wet, 120 °C); Permabond 801 (10–15 mPa·s, 0.05 mm, high temperature). For polypropylene, polyethylene, PTFE, and silicone, pretreatment with Permabond Polyolefin Primer (POP) is always required.
Your question not covered?
Our technical team provides personal advice on material selection, processing questions, and individual requirements. Fast and competent.
Product Specifications
| Product Information | |
|---|---|
| Container | 20 g or 50 g or 500 g |
| Manufacturer | Permabond Engineering Adhesives Ltd |
| Brand | Permabond |
| Country of origin | Italy |
| Tensile Strength | >20 N/mm² |
| UFI (Unique Formula Identifier) | Y5H0-3'7J-A00F-14R2 |
| Performance at Full Cure | |
|---|---|
| Shear strength polycarbonate | >6 |
| Dielectric strength | 25 kV/mm |
| Physical Properties | |
|---|---|
| Color | colorless |
| Chemical group | Ethyl Cyanoacrylate |
| Viscosity (adhesives) | Low viscosity <500 MPas |
| Viscosity mPa.s | 15-50 |
| Curing values | |
|---|---|
| Maximum gap fill (mm) | 0.1 |
| Fixture time on steel (sec.) | 2-3 |
| Hand Strength Rubber (sec.) | 2-3 |
| Hand Strength Phenol (sec.) | 2-3 |
| Final strength | 24 hours |
| Mechanical properties | |
|---|---|
| Hardness (Shore D) | 85 |
| Shear strength ISO 4587 in N/mm² | |
|---|---|
| Steel | 18-22 |
| ABS | >6 |
| PVC | >10 |
| Thermal Properties | |
|---|---|
| Operating temperature (°C) | -55 to +80 |
| Storage Temperature (°C) | 2-7 |
| Keywords | |
|---|---|
| Keywords | |
Documents and data sheets
Safety Data Sheets (SDS) and Technical Data Sheets (TDS) for download:
- Permabond 791 - Technical Data Sheet FR.pdf (340 KB)
- Permabond 791 - Fiche de Sécurité FR.pdf (334 KB)
- Permabond 791 - Safety Data Sheet EN.pdf (312 KB)
- Permabond 791 - Safety Data Sheet DE.pdf (335 KB)
- Permabond 791 - Technical Data Sheet EN.pdf (375 KB)
- Permabond 791 - Technical Data Sheet DE.pdf (334 KB)